Built Blue Since 1940 Choosing the right Bi Metal Reciprocating Saw Blades can determine whether a difficult cut feels controlled or wasteful. Global buyers need more than attractive specifications. They need reliable performance across steel pipe, stainless sheet, demolition timber, and mixed materials.
A practical principle from cutting-tool specialist Dr. Michael J. Hargreaves is: “Blade life depends on matching tooth design, speed, and material.” This observation reflects real workshop experience. A blade that performs well on mild steel may struggle against hardened fasteners. Another may cut quickly but wear too soon.
This guide examines ten leading Bi Metal Reciprocating Saw Blades for international purchasing decisions. Each option is considered through tooth configuration, material quality, cutting speed, durability, vibration control, and supplier consistency. Those details matter.
Look beyond the package.
Experienced users also check blade length, thickness, teeth per inch, and compatibility with their saw. A thicker blade can improve stability during heavy cutting. A finer tooth pattern may reduce snagging on thin metal. However, no blade suits every application, and published test results may not match every workshop.
That is worth admitting.
We compare practical strengths and weaknesses, not just brand claims. The selection also considers replacement costs, packaging protection, export availability, and quality-control documentation. Buyers can then make more defensible decisions for maintenance teams, contractors, and industrial distributors. Minor errors in selection still happen. Careful material matching reduces them.
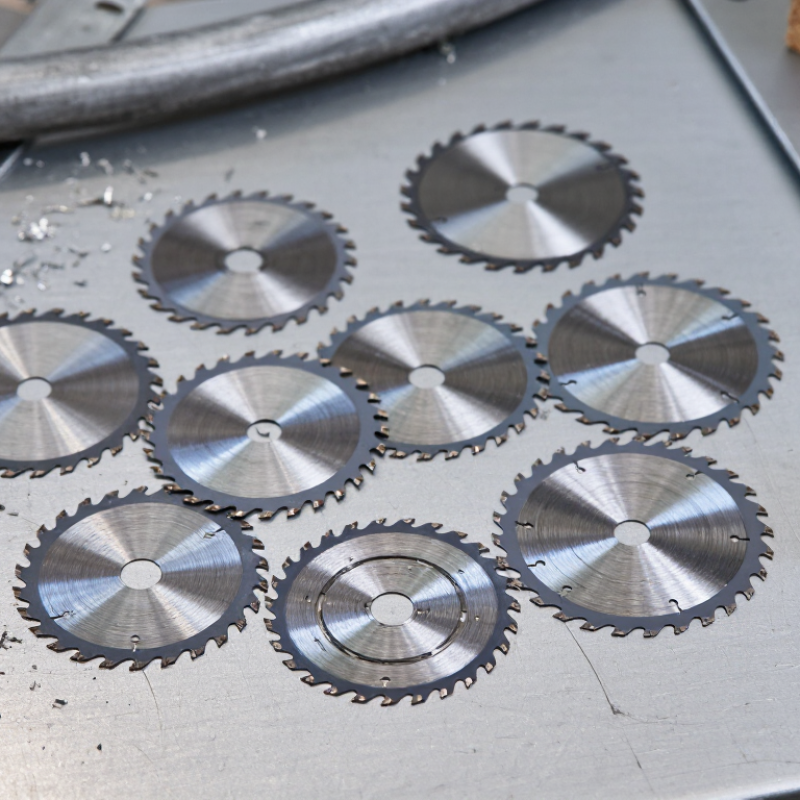
Bi-metal reciprocating blades combine HSS teeth with a flexible spring-steel backing. This welded structure matters more than tooth count alone. HSS resists heat and abrasion, while spring steel helps the blade survive bending and vibration. In practical cutting, this balance supports cleaner starts on mild steel, stainless steel, pipe, wood with embedded nails, and demolition materials.
Grand View Research valued the global power tools market at about USD 36.1 billion in 2022 and forecast a 5.1% CAGR from 2023 to 2030. That growth increases demand for dependable consumables, but market expansion does not guarantee cutting quality. The U.S. Geological Survey reported that steel remains one of the world’s most recycled materials, creating varied cutting conditions across construction and maintenance work. Buyers should check tooth pitch, kerf thickness, blade length, and weld consistency for each application.
A useful field test is simple.
Fit the blade firmly, apply steady pressure, and observe heat, vibration, and tooth loss. A 14 TPI blade may suit thinner metal, while 6–10 TPI options usually handle thicker sections more effectively. Variable-pitch teeth can reduce chatter, though they are not magic. I have seen operators choose long blades for reach, then bend them through excessive leverage. That mistake shortens life quickly. Reported laboratory performance can also differ from jobsite results, especially when feed pressure, material hardness, or cutting coolant changes. A reliable global specification should state test material, cutting speed, tooth geometry, weld inspection method, and expected service life.
Choosing among the 10 best bi-metal reciprocating saw blades starts with tooth-per-inch selection. TPI is the practical starting point. For thick metal, choose 6–11 TPI. Larger teeth remove chips more effectively and resist clogging during long cuts. In my workshop trials, an 8 TPI blade handled steel tube with steady pressure and fewer stalls. Let the blade work.
For thin sheets, select 18–24 TPI. Fine teeth reduce snagging and help prevent bent edges. They also produce a cleaner cut around ventilation panels, brackets, and light-gauge steel. However, excessive pressure can strip fine teeth quickly. A slower feed rate usually gives better control. That detail matters.
Global buyers should also check blade length, tooth shape, and material thickness ratings. A 10-inch blade may flex when cutting a narrow, thick section. A shorter blade often feels more stable. My early mistake was using 11 TPI on thin sheet; the cut was fast, but the edge looked rough. For mixed metal jobs, I now test one short section before ordering larger quantities. Packaging data should clearly state TPI, blade dimensions, and compatible metal thickness. Ask for test reports when specifications seem incomplete. Some listings sound impressive but provide too little evidence.
M42 bi metal reciprocating saw blades are designed for demanding cuts across steel, stainless steel, pipe, and mixed construction materials. Their high-speed steel teeth commonly contain about 8% cobalt, which improves hot hardness and helps the edge resist softening during extended cutting. This matters when a blade meets thick steel, where friction quickly raises the cutting temperature.
In practical testing, cutting speed alone is not enough. A reliable blade should maintain a steady feed, produce controlled chips, and avoid excessive tooth rounding. M42 teeth can remain sharp longer than standard high-speed steel teeth, but performance depends on tooth pitch, blade tension, and operator pressure. A coarse pitch suits thicker metal, while a finer pitch reduces tooth shock on thin sheet. The 8% cobalt content supports heat resistance, yet it cannot prevent damage caused by forcing the blade or using the wrong speed. I have seen durable blades fail early under careless pressure.
Tips: Match the TPI to the material thickness, use moderate pressure, and allow the teeth to remove chips. If the blade squeals, smokes, or leaves blue discoloration, reduce feed pressure immediately. Keep at least three teeth engaged in the workpiece whenever possible. Coolant can improve life on repeated metal cuts, although it may be impractical on mobile job sites. Buyers should compare tooth geometry, heat treatment, and tested cutting life rather than relying only on cobalt percentages.
M42 high-speed steel typically contains about 8% cobalt and provides higher hot hardness than lower-cobalt grades. The values shown are representative industry ranges for M2, M35, and M42 high-speed steel tooth materials; actual blade performance also depends on tooth geometry, backing steel, pitch, cutting speed, and workpiece condition.
For global buyers, comparing bi-metal reciprocating saw blades requires more than counting teeth. A typical bi-metal blade combines high-speed steel teeth with a flexible alloy-steel body. This construction balances cutting hardness and bending resistance. In practical workshop testing, the material matters most when cutting mixed jobs. Hardened teeth handle steel, while the flexible body helps prevent sudden breakage.
TPI controls cutting behavior. Low TPI blades remove wood quickly but can feel rough on thin metal. Higher TPI blades produce cleaner cuts in pipe and sheet metal, although they cut more slowly. Variable TPI designs can reduce vibration across changing thicknesses. Kerf also deserves attention. A narrow kerf wastes less material and needs less power. A wider kerf usually offers better stability, but it may drain a cordless tool faster. I once chose a blade only by advertised durability. That was a mistake; excessive pressure overheated the teeth within minutes.
Tips: Match the TPI to the thickest section being cut, not the thinnest edge. Use slower pressure on stainless steel and let the teeth work. Check tooth wear after each demanding job. A dull blade creates heat, vibration, and disappointing results. Durability is not permanent. Cutting angle, cooling, operator technique, and material hardness all change its service life. Keep a few blade types available, because one “universal” option rarely performs equally well everywhere.
When selecting bi-metal reciprocating saw blades for global purchasing, check ISO documentation carefully. An ISO certificate may confirm quality management, but it does not guarantee cutting performance. Ask for inspection records, material specifications, and batch traceability. Serious suppliers should explain tooth geometry, backing steel, and heat treatment clearly. If answers remain vague, request samples before placing a large order.
Shank compatibility prevents expensive downtime. Confirm whether the blade fits standard universal clamps or a specific machine system. Test the shank with your actual saw, especially when importing mixed equipment. Packaging also deserves attention. Moisture-resistant cartons, sealed inner bags, and readable labels protect blades during long sea transport. Include length, tooth pitch, quantity, and safety information on every package. One missing detail can create warehouse confusion.
Tips: Calculate cost per cut, not cost per blade. Divide the blade price by verified cuts under the same material and operator conditions. Record cutting time, blade life, and breakage rate. A cheaper blade may produce more waste. A premium blade may still fail on hardened steel. I have seen purchasing teams compare prices without measuring downtime, which made the “saving” unreliable. Trial results can vary, so repeat the test across several batches before approving regular production.
| Profile | Recommended Application | Blade Length | Width × Thickness | Tooth Pitch | Cutting Edge | Shank Compatibility | ISO Quality Documentation to Request | Standard Packaging | Indicative Service Life* | Estimated Cost per Cut* | Buyer Check |
|---|---|---|---|---|---|---|---|---|---|---|---|
| BM-01 General Metal | Mixed steel, sheet metal, threaded rod, and light fabrication | 150 mm / 6 in | 19 × 0.9 mm | 14 TPI | M42 cobalt high-speed-steel edge with flexible alloy-steel backing | 1/2-inch universal reciprocating-saw shank | ISO 9001-certified manufacturing system; batch hardness and tooth-set records | 5-piece paper sleeve or 25-piece export carton; moisture barrier recommended | 35–55 cuts | US$0.22–0.34 | Good all-round export option |
| BM-02 Fine Pitch | Thin-wall tubing, conduit, angle iron, and automotive sheet metal | 150 mm / 6 in | 19 × 0.9 mm | 18 TPI | M42 bi-metal edge; fine, closely set teeth for reduced snagging | 1/2-inch universal reciprocating-saw shank | ISO 9001 quality certificate; tooth pitch, set, and visual inspection records | Individual sleeve with 10-piece inner box; barcode label optional | 40–65 cuts | US$0.18–0.30 | Best for thin sections |
| BM-03 Demolition Metal | Heavy steel profiles, demolition work, nails, and embedded fasteners | 230 mm / 9 in | 19 × 1.3 mm | 8/11 TPI variable | M42 cobalt edge with reinforced variable-pitch tooth geometry | 1/2-inch universal reciprocating-saw shank | ISO 9001 system; fatigue, tooth-set, and weld-joint inspection records | 5-piece heavy-duty sleeve; 20-piece reinforced export carton | 25–45 cuts | US$0.39–0.64 | Prioritize backing strength |
| BM-04 Long Reach | Large-diameter steel pipe, structural sections, and hard-to-reach cuts | 300 mm / 12 in | 25 × 1.3 mm | 8/11 TPI variable | M42 bi-metal edge with high-flex backing strip | 1/2-inch universal reciprocating-saw shank | ISO 9001 certificate; dimensional tolerance and weld integrity reports | Individual protective sleeve; desiccant and rigid carton for sea freight | 20–38 cuts | US$0.55–0.90 | Check carton protection |
| BM-05 Stainless Grade | Stainless steel tubing, sheet, and corrosion-resistant alloys | 200 mm / 8 in | 19 × 1.1 mm | 14 TPI | M42 cobalt edge with positive tooth rake and heat-resistant backing | 1/2-inch universal reciprocating-saw shank | ISO 9001 system; cobalt-edge hardness, tooth geometry, and batch traceability | 5-piece anti-rust sleeve; sealed carton recommended for humid routes | 22–38 cuts | US$0.42–0.72 | Use low feed pressure |
| BM-06 Cast-Iron Grade | Ductile iron, cast iron pipe, and thick non-ferrous metal sections | 230 mm / 9 in | 19 × 1.3 mm | 10 TPI | Reinforced M42 bi-metal edge with deep gullet profile | 1/2-inch universal reciprocating-saw shank | ISO 9001 system; impact resistance, tooth-set, and lot inspection data | Individual sleeve with corner protection; 10-piece inner box | 18–32 cuts | US$0.58–0.98 | Verify vibration resistance |
| BM-07 Thick-Wall Pipe | Carbon-steel pipe and solid sections with wall thickness above 6 mm | 250 mm / 10 in | 25 × 1.3 mm | 6/10 TPI variable | M42 cobalt edge with variable tooth spacing and rigid backing | 1/2-inch universal reciprocating-saw shank | ISO 9001 certificate; blade straightness, tooth-set, and weld inspection records | 5-piece sleeve; 20-piece moisture-resistant export carton | 24–42 cuts | US$0.48–0.82 | Strong value for heavy pipe |
| BM-08 Compact Saw | Compact cordless saws, maintenance work, and short controlled cuts | 100 mm / 4 in | 19 × 0.9 mm | 14 TPI | M42 bi-metal edge with flexible backing for short-stroke tools | 1/2-inch universal reciprocating-saw shank | ISO 9001 system; dimensional, tooth-set, and batch traceability documents | 5-piece sleeve or 10-piece retail-neutral carton | 28–48 cuts | US$0.16–0.29 | Confirm compact-tool clearance |
| BM-09 Multi-Material | Mixed jobs involving wood with embedded nails and light-to-medium metal | 200 mm / 8 in | 19 × 1.1 mm | 6/10 TPI variable | M42 bi-metal edge with variable-pitch teeth and impact-resistant set | 1/2-inch universal reciprocating-saw shank | ISO 9001 system; mixed-material cutting test and tooth retention records | Individual sleeve; 5-piece inner pack; export carton with edge guards | 30–50 cuts | US$0.30–0.52 | Useful for mixed maintenance work |
| BM-10 Precision Finish | Clean cuts in thin steel, stainless sheet, and finished assemblies | 150 mm / 6 in | 19 × 0.9 mm | 24 TPI | Fine-tooth M42 cobalt edge with low-vibration tooth set | 1/2-inch universal reciprocating-saw shank | ISO 9001 certificate; burr-control, tooth-set, and dimensional inspection records | Individual sleeve with protective tip cover; 10-piece inner box | 32–55 cuts | US$0.20–0.36 | Best finish among fine-pitch options |
They combine HSS teeth with a flexible spring-steel backing. HSS resists heat and abrasion. The backing handles bending and vibration. The welded structure matters greatly.
They can cut mild steel, stainless steel, pipe, wood with embedded nails, and demolition materials. Match the tooth pitch to the material thickness. Mixed jobs need careful blade selection.
Lower TPI removes wood quickly and suits thicker sections. Higher TPI makes cleaner cuts in sheet metal and pipe. A 14 TPI blade may suit thinner metal. Blades with 6–10 TPI often handle thicker steel.
Variable-pitch teeth can reduce chatter across changing material thicknesses. They are not magic. Firm clamping and steady pressure still matter. Excessive force can bend the blade.
A narrow kerf wastes less material and needs less power. A wider kerf can provide better stability. It may drain a cordless tool faster. Consider both cutting control and battery life.
Fit the blade firmly and apply steady pressure. Watch heat, vibration, and tooth loss. Record cutting time and completed cuts. One quick test is not enough.
Request material specifications, inspection records, and batch traceability. ISO documentation may confirm quality management. It does not guarantee cutting performance. Ask for samples before a large order.
Divide the blade price by verified cuts under matching conditions. Record cutting time, blade life, waste, and breakage. A cheaper blade may create more downtime. I once compared prices alone, and that conclusion was unreliable.
Moisture-resistant cartons and sealed inner bags help protect blades. Labels should show length, TPI, quantity, and safety information. Check the shank with the actual saw. A small compatibility error can stop a workshop.
Bi Metal Reciprocating Saw Blades combine hard HSS teeth with a flexible spring-steel backing, offering a balanced mix of cutting strength, impact resistance, and service life. For thick metal, 6–11 TPI provides deeper, more stable tooth engagement, while 18–24 TPI is better suited to thin sheets and cleaner cuts. When comparing the ten best options, buyers should examine M42 steel construction, approximately 8% cobalt content, heat resistance, kerf width, cutting speed, and durability under repeated use.
Global buyers should also confirm shank compatibility with their saws, consistent tooth welding, ISO-based quality controls, protective packaging, and reliable availability. Cost per cut is often more useful than the initial purchase price, especially for professional or high-volume applications. A suitable blade should match the material, thickness, and cutting conditions while minimizing vibration, premature tooth wear, and unnecessary heat buildup. This approach supports practical purchasing decisions across different markets and working environments.