 Built Blue Since 1940
EN Contact Us
Built Blue Since 1940 Explore our premier line of CE-certified metalworking tooling, progressive stamping dies, and industrial thread-cutting accessories built for rigorous manufacturing environments.
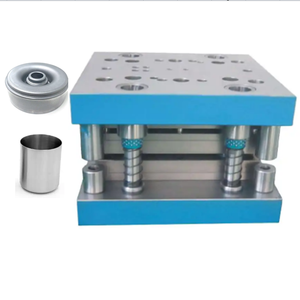
Custom heavy-duty metal punching molds and deep drawing die sets for automated sheet metal production lines.
Inquire Now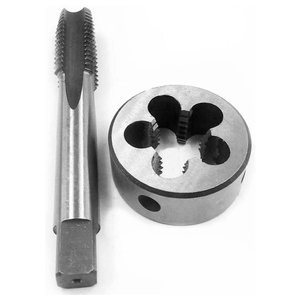
High-speed steel (HSS) right-hand tap and die combination set engineered for exact micro-thread cutting.
Inquire Now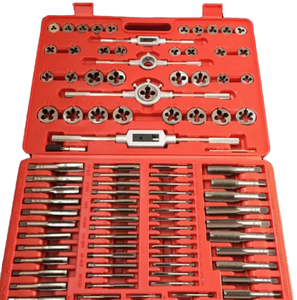
Comprehensive 110/86/60/45 piece alloy steel thread cutting tooling housed in heavy-gauge metal storage boxes.
Inquire Now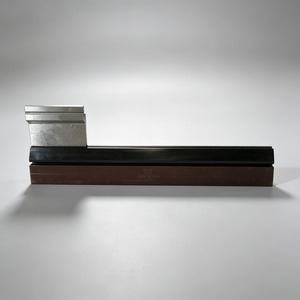
Vacuum heat-treated 42CrMo and H13 tool steel press brake punches and dies for CNC sheet metal bending machinery.
Inquire Now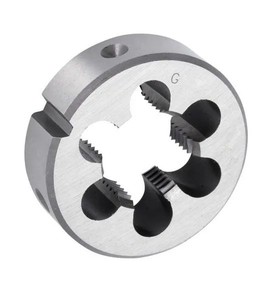
Titanium Nitride coated high-speed steel pipe thread cutter (D=45mm) designed for leak-free hydraulic joint threading.
Inquire Now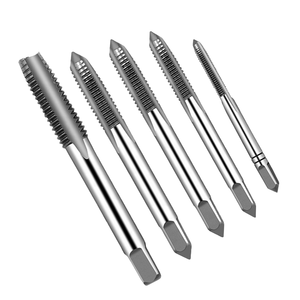
8-Piece high-wear-resistant titanium coated tap and die tooling kit for fast hand and machine threading operations.
Inquire Now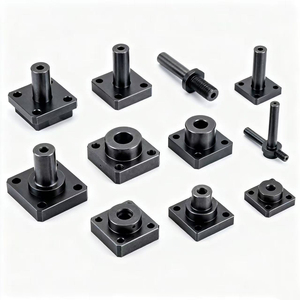
High-precision custom punching and shearing die sets engineered for multi-axis metal stamping operations.
Inquire Now
Precision-ground 2-piece UNC fractional tapping tools covering 3/8", 7/16", 1/2", and 9/16" sizes for heavy industrial repair.
Inquire NowIn high-speed sheet metal forming, automated punching, and precision thread cutting, the structural integrity of industrial tooling determines operational uptime. Since 1940, our enterprise has operated under the Built Blue standard—a engineering philosophy rooted in rigorous metallurgy, uncompromising geometric accuracy, and strict adherence to European Conformity (CE) directives under Machinery Directive 2006/42/EC and ISO 9001:2015 quality management systems.
As a leading CE Certified Die Set Factory & Supplier, we bridge the gap between raw metallurgical science and high-volume industrial application. Every die set, press brake punch, and high-speed steel thread cutter engineered within our state-of-the-art facility undergoes exhaustive destructive and non-destructive testing before reaching global OEM assembly lines.
We specify premium-grade tool steels including M2 (1.3343), M35/M42 Cobalt (1.3243), 42CrMo (1.7225), and H13 (1.2344). Vacuum heat treatment ensures deep martensitic grain refining without surface decarburization.
CNC profile grinding and slow-wire EDM cutting yield guide post concentricity within ±0.002mm and surface roughness down to Ra 0.2µm, eliminating punch misalignment and galling during rapid press cycles.
Full material mill certification, spectrographic alloy validation, 100% Rockwell hardness verification (HRC 58-64 depending on application), and complete batch code laser etching for ERP integration.
Selecting the optimal alloy and surface coating for metal stamping, press brake bending, and threading prevents catastrophic premature tool failure.
| Tooling Classification | Core Alloy Grade | Hardness Rating (HRC) | Recommended Surface Treatment | Target Workpiece Material | Cycle Life Index |
|---|---|---|---|---|---|
| Progressive Stamping Dies | D2 (1.2379) / SKD11 | HRC 60 - 62 | PVD TiCN (Titanium Carbonitride) | High-Tensile Steel, Stainless 304/316 | > 2,500,000 Strokes |
| CNC Press Brake Bending Dies | 42CrMo / 42CrMo4 | HRC 47 - 52 (Induction Edge) | Nitride Hardening (0.5mm Depth) | Structural Steel Plates, Aluminum Sheet | > 1,200,000 Bends |
| Heavy-Duty Deep Drawing Tooling | H13 (1.2344) Premium | HRC 52 - 56 | TD (Thermal Diffusion) / DLC Coating | Deep-Draw Carbon Steel, Brass, Copper | > 1,800,000 Strokes |
| Precision Micro Taps & Dies | HSS-Co M35 (5% Cobalt) | HRC 65 - 67 | TiN (Titanium Nitride) Gold Finish | Inconel, Titanium, Hardened Alloy Steel | > 500,000 Threads |
| General Purpose Threading Tools | M2 HSS (1.3343) | HRC 63 - 65 | Steam Oxide / Bright Polished Flutes | Mild Steel, Cast Iron, Plastics, Wood | > 350,000 Threads |
As global supply chains shift toward digitalized Smart Manufacturing and Industry 4.0 architectures, procurement managers and OEM buyers are adopting stringent criteria when evaluating die set manufacturers. Purchasing decisions are no longer governed solely by unit price; instead, total cost of ownership (TCO), tooling longevity, real-time sensor compatibility, and environmental compliance are paramount.
The metal stamping and press brake tooling industry is experiencing a technological renaissance driven by advancements in materials science, laser surface texturing, and automated CNC grinding technologies. Understanding these micro-trends allows tooling engineers to optimize die performance for next-generation ultra-high-strength steels (UHSS) and lightweight magnesium alloys.
Combining plasma nitriding with multi-layer AlTiN or Diamond-Like Carbon (DLC) nanocomposite coatings increases surface hardness above HV 3000, drastically reducing friction and eliminating lubricant usage in dry-stamping applications.
Direct Energy Deposition (DED) 3D printing is integrated into conventional tool steel die bases to create 3D conformal cooling channels, reducing thermal stress during hot stamping of automotive B-pillars.
Micro-texturing die cavity surfaces creates microscopic lubricant reservoirs that prevent oil film breakdown under extreme contact pressures (>1000 MPa), extending deep drawing die life by 300%.
Direct, expert answers to critical technical and purchasing inquiries encountered by OEM procurement officers and tooling engineers.
CE certification for die sets compliance falls under the European Union Machinery Directive 2006/42/EC and harmonized safety standards EN ISO 12100:2010. It verifies that the die set assembly includes mechanical pinch-point risk reduction, safe lifting eyebolt load verification, pressure-relief safety features for gas springs, and structural finite element analysis (FEA) proving the bolster plates can withstand 150% rated press tonnage without structural fracture.
Choose 42CrMo for standard sheet metal bending tools up to 6mm plate thickness where high toughness and cost-effectiveness are required. Select D2 for high-volume progressive blanking and piercing dies where high wear resistance is needed against abrasive steels. Specify H13 for extreme-impact operations, thick plate bending, or hot stamping die sets where high thermal fatigue resistance and red hardness (up to 550°C) are non-negotiable.
Our CE certified die sets utilize precision ball guide or solid bronze sliding guide assemblies engineered to ISO 9182 / DIN 9825 standards. Guide pillar concentricity and diameter tolerance are held to h4/g3 limits (within 0.002mm - 0.004mm). Parallelism between top and bottom bolster plates is precision-ground within 0.005mm per 300mm length, ensuring absolute alignment for micro-punching operations down to 0.1mm thickness.
Yes. Our engineering division operates advanced 5-axis CNC machining centers, slow-wire EDM cutting machines, and surface grinding rigs linked directly to SolidWorks, Mastercam, and UG NX CAD/CAM suites. Customers provide 3D CAD files (STEP, IGES, X_T) or physical part samples. We perform full strip layout optimization, stamping simulation analysis (AutoForm), and manufacture custom progressive or compound dies tailored to your specific press tonnage and bed dimensions.
We provide complete OEM branding solutions for industrial tool distributors, automotive aftermarket groups, and hardware buying cooperatives. Options include custom laser marking of part numbers and logos directly onto tools, private-label color index cases, anti-corrosive VCI vacuum sealing, heavy-gauge wooden crate packaging for ocean freight, and full EDI integration for automated dropshipping to regional distribution hubs worldwide.
Whether you require standard stock press brake tooling, high-speed steel tap & die sets, or turnkey custom progressive stamping dies, our engineering team is standing by to review your CAD files and technical specifications.
Inquire Now