 Built Blue Since 1940
EN Contact Us
Built Blue Since 1940 Explore our high-performance industrial punching dies, abrasive prep wheels, and heavy-duty perforation components manufactured under strict ISO 9001:2015 quality standards.

Low-noise precision abrasive flap assembly equipped with reinforced steel shaft for high-speed metal edge deburring and hole finishing.

Ultra-thin industrial cut-off disc designed for clean plate shearing, burr-free hole trimming, and stainless steel fabrication.

Fine-grit aluminum-core diamond wheel engineered for re-sharpening tungsten carbide punch dies and refining internal cylinder bores.

Heavy-duty segment surface grinding wheel for structural substrate preparation, concrete opening cleanout, and tough alloy beveling.

Wholesale industrial-grade abrasive grinding wheel formulated for alloy steel conditioning, flash removal, and die neck shaping.

Factory-direct 24#~80# grit angle grinder wheel optimized for sheet metal perforation relief cuts and fast stock removal.

Aluminum oxide Grit 80 precision regulating wheel engineered for high-accuracy cylindrical punch pin grinding and rod tolerance sizing.

Sintered matrix double-row diamond wheel for heavy masonry hole edge chamfering, flash cleanup, and high-abrasion material processing.
Comprehensive technical analysis of tooling metallurgy, hydraulic stroke mechanics, and high-tonnage perforation engineering for enterprise procurement managers.
Over the past two decades, China has evolved from a volume-centric hardware manufacturer into the worldwide epicentre for high-precision metal perforation systems, custom hydraulic punch dies, and automated CNC tooling assemblies. Modern industrial buyers no longer evaluate a China hole punch factory purely on unit cost; today’s global supply chain demands rigorous metallurgical traceability, micron-level dimensional repeatabilities, and optimized shear geometry designed to minimize press machine fatigue.
At the core of top-tier Chinese punch manufacturing is the integration of premium tool steel metallurgy—utilizing materials such as Cr12MoV, Japanese SKD11, Swedish Vanadis 4 Extra, and Premium Tungsten Carbide (WC-Co). By applying vacuum heat treatment and multi-stage cryogenic stabilization, leading exporters ensure that punch pins and matrix dies maintain structural integrity under dynamic impact loads exceeding 500 metric tons.
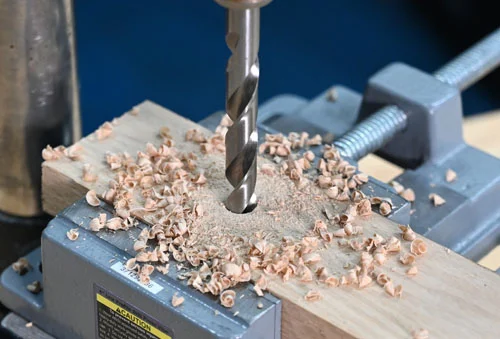
Selecting the optimal punch pin steel grade and die clearance parameter is vital for maximizing tooling cycle life and preventing burr formation.
| Steel / Tooling Grade | Hardness (HRC) | Yield Strength (MPa) | Recommended Substrate | Expected Stroke Life | Primary Industrial Application |
|---|---|---|---|---|---|
| Cr12MoV (China GB) | 58 - 60 HRC | 1,650 MPa | Mild Steel, Aluminum, Brass | 300,000 - 500,000 | Standard HVAC ducting, electrical enclosure punching. |
| SKD11 / D2 (JIS / AISI) | 60 - 62 HRC | 1,850 MPa | Stainless 304/316, Structural Steel | 600,000 - 1,000,000 | Heavy sheet metal fabrication, automotive brackets. |
| DC53 (Daido Alloy Steel) | 62 - 64 HRC | 2,100 MPa | Hardened Spring Steel, High-Tension Alloy | 1,200,000 - 1,800,000 | High-speed CNC turret punch presses, continuous stamping. |
| HSS M2 / M35 (Cobalt) | 63 - 66 HRC | 2,400 MPa | Abrasive Composite, Thick Plate Steel | 2,000,000+ | Heavy hydraulic beam punch systems, thick pipe perforation. |
| Tungsten Carbide (K30/K40) | 88 - 92 HRA | 2,800 MPa | Thin Film Metal, Printed Circuit Boards | 5,000,000+ | Micro-perforation, electronics, high-speed rotary punch dies. |
*Note: Stroke life estimates reflect continuous production runs with automated coolant lubrication and calibrated die clearance.*
Integrating heritage tooling expertise with state-of-the-art CNC machining infrastructure to provide turnkey OEM/ODM industrial solutions.
Tracing our engineering legacy back to 1940 (built upon the legendary Century Drill & Tool industrial standards), we combine over 8 decades of cutting and punching experience with modern computer-simulated FEA shear dynamics.
Our facility houses 5-axis Swiss CNC lathes, Makino wire-EDM systems, and Okamoto surface grinders capable of achieving pin tolerances down to ±0.002mm and concentricity within 0.001mm.
Every batch undergoes automated Zeiss CMM dimensional verification, Rockwell hardness testing, and digital optical projector checks. Full metallurgical material test certificates (MTC) are issued per EN 10204 3.1 standards.
From complex progressive stamping dies to specialized hydraulic angle-iron notchers, our dedicated R&D engineering team transforms your 2D/3D CAD models (STEP, IGES, DXF) into production-ready physical tooling in under 15 days.
In-house PVD coating chambers allow custom deposition of TiN, TiAlN, CrN, and AlCrN coatings tailored to your specific workpiece friction coefficient and operating temperature requirements.
Robust logistics network with custom VCI anti-rust packaging, export-ready wooden crating, and seamless integration with DDP, FOB, and CIF maritime shipping to North America, Europe, and Southeast Asia.
As smart manufacturing initiatives accelerate globally, the procurement landscape for industrial hole punching tools and press equipment is undergoing a major paradigm shift. B2B sourcing executives must align their supply chains with four critical emerging trends:
Modern high-speed punching presses are increasingly integrated with strain gauges and acoustic emission sensors embedded directly within the die sets. Chinese exporters leading the market now supply punch units prepassed for smart condition monitoring, enabling predictive maintenance before catastrophic die chipping occurs.
Environmental compliance (RoHS, REACH) has made Eco-PVD coatings non-negotiable. Modern factories are replacing older hexavalent chrome electroplating processes with closed-loop magnetron sputtering, resulting in zero toxic byproduct emissions while extending tool edge life by up to 40%.
To reduce downtime during low-volume, high-mix production runs, global manufacturers are demanding ISO-standardized quick-change punch holders. Standardized ball-lock mechanisms and pneumatic clamp adapters allow tool changes in under 90 seconds, dramatically increasing overall equipment effectiveness (OEE).
Clear, definitive technical answers curated by our senior tooling design engineers and quality assurance directors.
Tonnage requirements are calculated using the formula: $\text{Force (Tons)} = \frac{\text{Perimeter of Hole (mm)} \times \text{Material Thickness (mm)} \times \text{Shear Strength (N/mm}^2\text{)}}{9806.65}$. For instance, punching a 20mm round hole in 3mm thick mild steel (shear strength $\approx 400 \text{ N/mm}^2$) requires approximately 7.7 metric tons of pressing force. Introducing a roof shear angle to the punch tip can reduce the peak tonnage requirement by up to 30-50%.
For stainless steel (304, 316, or 410 grade), total clearance should typically be set between 10% and 15% of the material thickness ($T$). Setting the clearance too tight drastically increases punching force and accelerates punch edge wear, whereas excessive clearance causes excessive burrs, rollover zones, and heavy tensile fracture along the slug cut line.
We mitigate pin failure by utilizing vacuum heat-treated Japanese SKD11 or DC53 tool steel, incorporating a 2-stage back-taper (0.01mm to 0.03mm) along the punch body to eliminate galling, and radius-blending all internal corner transitions. Furthermore, stress-relief tempering is performed three consecutive times following EDM wire cutting.
Yes. Our engineering division works directly with STEP, IGES, DWG, and SolidWorks CAD files. We provide full DFM (Design for Manufacturing) reports prior to production, verifying clearance parameters, spring stripper selection, and material grain direction to optimize your tooling longevity.
Standard prototype punch pins and standard matrix dies are produced within 7 to 10 working days. Complex progressive stamping dies or complete hydraulic punching head units generally require 20 to 30 days, inclusive of CMM inspection and initial sample testing (T1 trial runs with full inspection reports).
All finished steel tooling components undergo automated ultrasonic cleaning, application of high-viscosity VCI (Vapor Corrosion Inhibitor) protective oil, vacuum poly-bagging, and secure placement inside heavy-duty foam-lined plywood cases certified for sea and air freight.
Every shipment is accompanied by a comprehensive Quality Documentation Package containing EN 10204 3.1 Metallic Material Test Certificates (verifying chemical composition and tensile strength), CMM Dimensional Inspection Reports, Heat Treatment Hardness Validation Certificates, and ISO 9001:2015 Compliance Sheets.
We operate under a strict Quality Guarantee standard. In the rare event of a dimensional mismatch or material failure outside specified drawing tolerances, our team dispatches replacement tooling via priority air courier within 48 hours at zero cost to the client, backed by an immediate root-cause CAPA investigation.
Request a comprehensive tooling catalog, schedule a technical consultation with our engineering team, or submit your CAD drawings for an instant competitive quotation.
Send an Inquiry