 Built Blue Since 1940
EN Contact Us
Built Blue Since 1940 Engineered for high-volume metal stamping, electrical panel knockout, structural steel fabrication, and precision hole finishing across Greater Mexico City.
Analyzing the Nearshoring Boom, Hydraulic Tooling Demands, and Precision Punch Manufacturing in Central Mexico’s Manufacturing Corridors.
As Mexico City (CDMX) solidifies its position as the premier financial and light-to-heavy industrial nerve center of Central Mexico, manufacturing facilities in Industrial Vallejo, Iztapalapa, Naucalpan, Tlalnepantla, and the Toluca industrial belt face unprecedented demand for rapid-cycle metal fabrication tooling. Driven by the USMCA (T-MEC) framework and accelerating nearshoring investment, regional tier-1 automotive suppliers, electrical enclosure manufacturers, and structural fabricators require industrial-grade hole punch dies, hydraulic knockout punches, and CNC turret tooling capable of enduring rigorous multi-shift operation.
Selecting the optimal hole punch factory or vendor requires a deep understanding of localized manufacturing stresses. Standard off-the-shelf punch dies frequently suffer from premature edge chipping, slug pulling, and thermal deformation when subjected to Mexico City’s distinct operational variables, including high ambient elevation dynamics (2,240 meters above sea level) affecting pneumatic stroke speeds, and intense micro-alloy steel work-hardening rates.
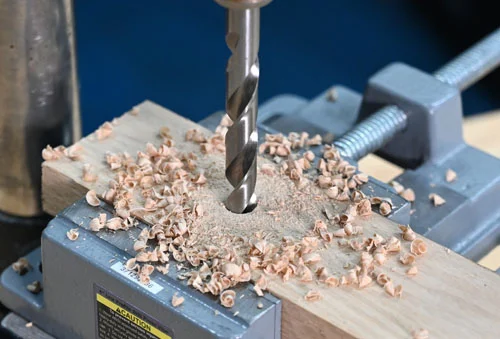
In high-throughput fabrication plants across Mexico City, converting high-volume hole-making operations from conventional rotational drilling to hydraulic or mechanical punching reduces operational cycle times by up to 82%. While twist drilling relies on chip removal via rotational friction—generating excessive localized thermal stress—punching utilizes instantaneous shear displacement. Implementing precision-ground punch-and-die sets with controlled clearances (8% to 12% of material thickness) eliminates secondary deburring steps and drastically lowers per-hole cost in structural I-beams, C-channels, and sheet metal panels.
Matching Tool Steel Metallurgy, Shear Angles, and Die Clearances to Substrate Toughness for Zero-Defect Production.
Engineered for electrical contractors and panel builders in CDMX. Three-point split-slug punch geometries allow clean conduit knockouts in up to 3.5mm mild steel and stainless enclosures without distorting the surrounding panel profile.
Fully compatible with Thick Turret, Thin Turret, and Trumpf-style punch presses. Features Titanium Nitride (TiN) and TiCCN PVD coatings that prevent material galling when punching galvanized and aluminum sheet alloys.
Designed for bridge girders, commercial architectural frames, and heavy equipment chassis. Manufactured from shock-resistant S7 tool steel to withstand extreme impact force without catastrophic cracking.
| Workpiece Substrate | Material Thickness | Recommended Punch Steel | Optimal Die Clearance | Shear Profile Type | Calculated Force Factor |
|---|---|---|---|---|---|
| Mild Steel (A36 / SPCC) | 1.5mm – 6.0mm | M2 High-Speed Steel | 10% of Thickness | Flat Shear / Rooftop | 25 – 35 kg/mm² |
| Stainless Steel (304 / 316) | 1.0mm – 4.0mm | M35 Cobalt / Powder Metallurgy | 12% – 15% of Thickness | Double Bevel (Rooftop) | 55 – 68 kg/mm² |
| Aluminum Alloy (5052-H32) | 1.0mm – 8.0mm | D2 Tool Steel (TiN Coated) | 6% – 8% of Thickness | Flat / Micro-Shear | 15 – 22 kg/mm² |
| Copper / Brass Busbars | 2.0mm – 10.0mm | Cr12MoV / M2 HSS | 5% – 7% of Thickness | Polished Flat Face | 20 – 28 kg/mm² |
| Structural Plate (AH36) | 6.0mm – 20.0mm | S7 Shock-Resistant Steel | 12% – 18% of Thickness | High-Shear Concave | 45 – 58 kg/mm² |
Custom Engineering Solutions Tailored to the Specific Production Workflows of Central Mexico’s Leading Sectors.
High-speed production punches designed for automotive bracketry, structural chassis components, and heat shield perforations. High-cycle tooling delivers up to 500,000 hits before re-sharpening.
Standard ISO metric and conduit-sized hydraulic knockout punches engineered for rapid panel installation. Leaves smooth, burr-free edges that meet strict IP66 and NEMA enclosure standards.
Portable hydraulic punch units and hand-held hole cutters for rapid site installation across Mexico City urban commercial construction projects, facilitating quick ducting and cable tray pass-throughs.
Custom OEM punch manufacturing for international machinery builders assembling equipment within Mexico for re-export under North American supply chain regulations.
For over eight decades, Century Drill & Tool has set the benchmark for industrial cutting, punching, and threading technology. Our enterprise tooling division combines legacy metallurgy expertise with state-of-the-art CNC grinding technology to deliver punches that exceed international ISO and ANSI specs.
Every batch of punches undergoes optical profile measurement and Rockwell C hardness verification, eliminating out-of-tolerance batch variations.
Punches feature specialized ejector pins, urethane strippers, and micro-tapered relief geometries that eliminate slug pulling in high-speed automated presses.
Streamlined customs clearance and direct logistics routing ensure door-to-door delivery within 24 to 48 hours for emergency tooling replacements in CDMX.
Combining Precision Punching with Advanced Abrasives for Seamless Sheet Metal Finishing.
Achieving flawless hole punching requires more than just a sharp punch-and-die set. Surface scale, rust, and oil coatings can cause punch slippage and uneven die wear. Century Drill & Tool provides an end-to-end ecosystem of industrial abrasives, including flap wheels, Type 1 cutting discs, and double-row diamond grinding cups to prepare sheet surfaces before punching.
Following the punching operation, heavy-duty deburring using non-woven abrasive wheels or shaft-mounted flap wheels ensures that sharp burrs, rollover zones, and micro-fractures are smoothed out prior to powder coating or plating, preventing paint adhesion failure in industrial enclosures.
Direct Answers to Critical Questions Regarding Punch Selection, Local Shipping, Custom Tooling, and Die Maintenance.







