Top Trusted Threading Tap Manufacturers & Manufacturer Serving Seoul

Precision Engineering, Advanced PVD Coatings, and High-Speed Steel Threading Solutions for Seoul’s High-Tech Machining & Manufacturing Sectors

Precision Industrial Threading Taps

Engineered to DIN, ISO, and JIS Standards for High-Yield CNC Tapping & Manual Threading Operations

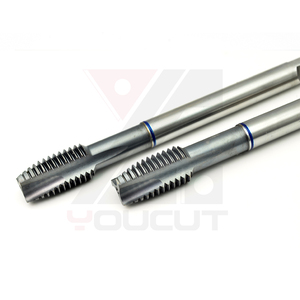
DIN Standard M12 Fine Thread HSSE Spiral Point Tap TiCN Coated
DIN Standard M12*1-M20*2 Fine Thread HSSE Spiral Point Tap TiCN Coated
Material: HSSE (M35 Cobalt) | Target: Stainless Through Holes
Send an Inquiry
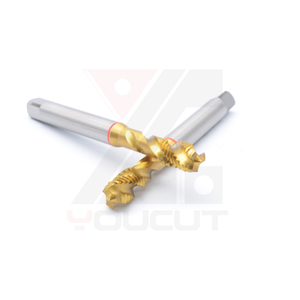
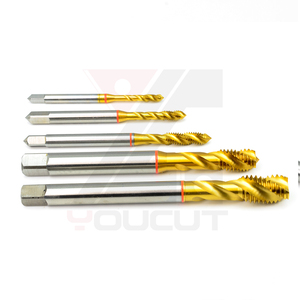
TiN Coated Tap HSSE Tap DIN Standard Spiral Flute Threading Tools
TiN Coated HSSE DIN Standard Spiral Flute Threading Taps M12-M20
Material: HSSE + TiN | Target: Stainless Steel Blind Holes
Send an Inquiry
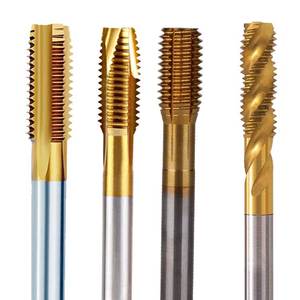
Amony HSS Cobalt 5% With Tin Coating Threading Machine Taps M35
M35 HSS-Co 5% TiN Coated Metric Machine Taps (Spiral/Point/Straight)
Material: M35 High-Speed Steel | Multi-Groove Options
Send an Inquiry
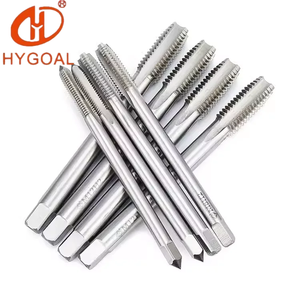
HYGOAL OEM Custom HSS Straight Flute Machine Tap Metric
HYGOAL OEM Custom HSS Straight Flute Metric CNC Tapping Tools
Material: Premium HSS | Target: Cast Iron & Structural Steel
Send an Inquiry
HSSE Spiral Flute Tap Set M2-M10 TiN Coated Tap DIN Standard
HSSE Spiral Flute Micro Tap Set M2*0.40 - M10*1.50 TiN Coated DIN
Material: HSSE | Target: Micro Precision & Stainless Blind Holes
Send an Inquiry
Professional Straight Flute Thread Machine Tap HSS Taper Pipe Thread
Professional HSS Straight Flute Machine Taps & Taper Pipe Taps
Material: HSS | Target: NPT/RC Pipe Threading & General Metal
Send an Inquiry
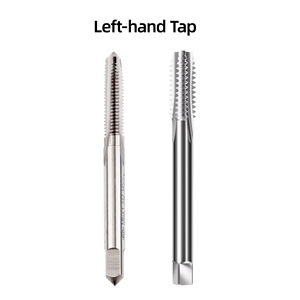
Left Hand Tap Reverse Thread Tap Drill Bit Machine Hand Tap Carbide
Left-Hand Reverse Thread Machine/Hand Taps M7-M9 Carbide/HSS
Material: Carbide / HSS | Target: Reverse Threading & Repairs
Send an Inquiry
Wholesale Threading HSS Machine Spiral Flute Taps Aluminium
High-Speed Steel Spiral Flute Machine Taps for Aluminium & Non-Ferrous
Material: Polished HSS | Target: Ductile Aluminium Alloys
Send an Inquiry
85+
Years Tooling Heritage (Built Blue Since 1940)
H6 / 6H
Micron-Level Pitch Diameter Precision Tolerance
5% Co
M35/HSSE Cobalt Content for Hardened Alloys
100%
Optical & Hardness Verification Quality Guarantee

Industrial Threading Tap Manufacturing Excellence for the Seoul Metropolitan Area

In the high-density manufacturing corridors of the Greater Seoul area—spanning key precision hubs such as Gasan Digital Complex, Seongsu-dong industrial workshops, and the nearby manufacturing centers of Incheon, Banwol, and Sihwa—the demand for high-reliability cutting and threading tools is paramount. As modern CNC machining centers run at higher surface speeds (V_c) and aggressive feed rates, threading taps undergo extreme thermal and mechanical stresses. A micro-fracture or chip-clogging event in a threading operation does not merely ruin the tap; it risks scrapping expensive, fully-machined components made from SUS304, SUS316L stainless steel, or titanium alloys.

As a global leader in high-performance cutting tools with an lineage dating back to 1940 under our Built Blue standard, our organization serves as a primary OEM partner and direct manufacturer supporting Seoul’s tier-1 automotive component suppliers, semiconductor equipment fabricators, and heavy machinery workshops. Delivering true Information Gain to tool buyers, process engineers, and procurement managers in South Korea requires moving beyond basic catalog specs to analyze the metallurgical, geometrical, and tribological parameters that govern thread creation.

Core Engineering Principle: Successful internal thread production depends on matching the tool's helix geometry and substrate hardness to the tensile strength and chip formation characteristics of the workpiece material. Incorrect chip evacuation geometry is responsible for over 78% of catastrophic tap breakages in automated CNC setups.

Technical Analysis: Tap Substrates, Geometries, and Coating Science

To withstand the rigorous demands of Seoul’s automated manufacturing infrastructure, our threading taps utilize premium-grade metallurgy combined with precise physical vapor deposition (PVD) surface coatings. Understanding the distinctions between substrate classes and flute geometries allows tool engineers to maximize tool life while minimizing cost per threaded hole.

1. High-Speed Steel Substrates: M2, M35 (HSSE), and Solid Carbide

The choice of substrate determines toughness, red hardness, and wear resistance:

  • Standard HSS (M2 / W6Mo5Cr4V2): Provides exceptional impact toughness and flexural strength. Ideal for general-purpose structural steel, carbon steel (S45C), and structural iron where vibration or spindle deflection is present.
  • M35 Cobalt HSS (HSSE / HSS-Co5%): Enriched with 5% Cobalt, M35 steel increases red hardness significantly, retaining edge sharpness up to 600°C. Recommended for work-hardening materials such as austenitic stainless steel (SUS304/316) and heat-resistant alloys.
  • Solid Micrograin Carbide: Offers ultra-high hardness (HRC 65+) and rigidity. Designed for high-volume automated CNC tapping of abrasive materials like cast iron (FC/FCD series), high-silicon aluminum, and pre-hardened die steels.

2. Advanced PVD Coatings for Friction Control

Uncoated taps frequently suffer from micro-welding and Built-Up Edge (BUE) formation when processing sticky materials. Our specialized surface treatments combat these failure modes:

Coating Type Microhardness (HV) Max Working Temp Coeff. of Friction Best Workpiece Application
TiN (Titanium Nitride) 2,300 HV 600°C 0.40 General carbon steels, alloy steels, copper, brass, standard blind-hole tapping.
TiCN (Titanium Carbonitride) 3,000 HV 400°C 0.25 Stainless steel (SUS304/316), tough alloy steels, abrasive materials requiring low friction.
AlTiN / TiAlN 3,300 HV 800°C 0.35 High-speed dry tapping, nickel-based superalloys, hardened steels up to HRC 45.
Bright / Polished Finish Uncoated Base 300°C 0.50 Ductile aluminum alloys (AL6061, AL7075), soft copper, plastic materials where coating adhesion is not optimal.

Geometrical Dynamics: Matching Flute Type to Hole Configuration

Selecting the correct flute structure is the most critical decision in tap selection. Internal threads fall into two main geometric categories: Through Holes and Blind Holes.

SP

Spiral Point Taps (Gun Taps)

Designed strictly for Through Holes. The angular point shoots chips forward ahead of the cut, preventing flute clogging. Offers high structural strength due to shallow straight flutes.

SF

Spiral Flute Taps

Engineered for Blind Holes. Helical flutes (typically 35° to 45° helix angle) pull chips upward out of the hole, preventing accumulation at the bottom that causes tap breakage.

ST

Straight Flute Taps

Versatile solutions for short-chipping materials like cast iron, brass, and hardened steel. Excellent for hand tapping or rigid CNC tapping setups requiring maximum thread stability.

Localized Industrial Application Scenarios in Seoul & Surrounding Tech Hubs

South Korea’s manufacturing ecosystem relies heavily on tight delivery timelines, strict quality control (ISO 9001/IATF 16949 compliance), and extreme precision. Our custom and standardized tap configurations serve key localized sectors across Greater Seoul:

1. Semiconductor Equipment Fabrication (Gasan & Pangyo Tech Valleys)

Semiconductor manufacturing chambers and gas distribution blocks rely heavily on high-purity SUS316L stainless steel and aluminum 6061 components. Tapping small thread sizes (M2 to M6 fine pitch) in work-hardening SUS316L requires our M35 HSSE TiCN-coated spiral flute taps. These tools feature optimized relief angles to minimize cutting torque and eliminate thread burrs, meeting the cleanroom cleanliness specifications required by major semiconductor OEMs in Gyeonggi-do.

2. Automotive Power-Train & EV Component Machining (Incheon & Banwol Hubs)

As South Korea accelerates its transition toward Electric Vehicles (EVs), lightweight aluminum battery enclosures and motor housings require rapid, reliable thread tapping. Our bright-finished spiral flute taps designed specifically for aluminum alloys feature polished flutes and specialized rake geometry that prevents aluminum micro-welding, allowing operating speeds up to 35 m/min on high-speed CNC machining centers.

3. Precision Prototype & Medical Device Manufacturing (Seongsu & Yeouido Suppliers)

Seoul’s vibrant medical device and precision instrument workshops require ultra-precise pitch tolerances (6H/ISO2 standards) for titanium grade 5 (Ti-6Al-4V) and cobalt-chrome implants. Our left-hand reverse taps, micro-pitch taps, and form taps deliver zero-chip cold-forming performance, ensuring thread integrity without micro-cracking in medical implants.

Key Manufacturing & Supply Trends in South Korea's Threading Market

Procurement strategies among Korean machine shops have evolved significantly over recent years. Understanding these technological trends helps Seoul purchasing agents stay competitive:

  1. Transition from Thread Cutters to Cold Form Taps (Roll Taps): In high-volume automotive and electronics manufacturing, cold forming taps—which shape threads via plastic deformation without creating chips—are replacing cutting taps. Form taps increase thread shear strength by up to 20% and completely eliminate chip disposal issues.
  2. Demand for DIN and JIS Standard Dual Compatibility: While international machinery imported into Seoul often follows DIN standards (DIN 371 / DIN 376), domestic equipment historically adheres to JIS (Japanese Industrial Standards). Our enterprise provides dual-standard inventory to allow seamless tool replacement across mixed-origin machinery fleets.
  3. Micro-Threading Solutions for Compact Electronics: With smart devices and wearable technology shrinking in size, thread sizes down to M0.8 and M1.2 with sub-micron tolerances have seen a 45% surge in local Seoul procurement requests.

Enterprise E-E-A-T Capabilities: Why Engineers & Buyers Partner With Us

Since 1940, our company has maintained a reputation built on manufacturing integrity, technical transparency, and continuous metallurgical research. As a global supplier serving industrial buyers in Seoul, we maintain rigorous quality assurance standards:

  • 100% Optical Inspection: Every batch of taps undergoes automated 3D optical profile checking for pitch error, thread profile angle, and concentricity before shipment.
  • Certified Metallurgical Sourcing: We source premium M2 and M35 HSS raw materials exclusively from certified steel mills, providing full heat-treatment traceability for industrial audit compliance.
  • Custom OEM & Pitch Tailoring: Need non-standard pitch diameters, special shank lengths for deep-cavity dies, or proprietary coating combinations? Our engineering team designs custom tooling drawings within 24 hours.

Localized Procurement & Technical FAQ

Direct Answers to Common Questions Asked by Machine Shop Managers in Seoul and Gyeonggi-do

What tap material and coating should I select for processing SUS304 stainless steel in Seoul machine shops?
For austenitic stainless steel like SUS304 or SUS316, we strongly recommend specifying M35 HSSE (5% Cobalt) taps with a TiCN coating. SUS304 work-hardens rapidly under friction. Cobalt provides the necessary red-hardness to resist thermal breakdown, while TiCN coating provides a low coefficient of friction (0.25) to prevent chip weld-on and premature tooth chipping.
How do DIN standard shanks differ from JIS standard shanks commonly used in South Korea?
DIN standard taps (such as DIN 371 for small sizes and DIN 376 for larger sizes) feature different overall lengths, shank diameters, and drive square dimensions compared to JIS B 4430 standards. While CNC collet holders can often accommodate both if correct collets are selected, standard tap wrenches and rigid tap holders must match the shank standard. We supply both DIN and JIS standard taps to fit your specific tooling setups.
What is the lead time for direct wholesale delivery of threading taps to Seoul or Incheon ports?
Standard catalog items (including metric spiral flute, spiral point, and straight flute taps in standard H-limits) ship within 24 to 48 hours. Air freight deliveries directly to Seoul (ICN / Incheon International Airport) typical take 3 to 5 business days, while bulk sea freight orders reach Incheon Port within 7 to 12 days depending on custom clearing protocols.
Why do my taps break prematurely when threading blind holes in high-speed CNC centers?
Blind hole breakage is usually caused by using straight flute or spiral point taps instead of spiral flute taps, leading to chip compaction at the bottom of the hole. Other contributing factors include improper drill pre-hole diameter (hole size too small, loading the tap beyond 75% thread depth) or excessive run-out in the tool holder. Ensure your pre-drill size matches standard pitch tables (e.g., Ø10.2mm pre-drill for M12x1.75).
Can you manufacture custom pitch left-hand taps or specialized micro-taps for OEM programs?
Yes. We provide complete OEM and custom tooling design programs. We manufacture left-hand reverse thread taps, specialized fine-pitch metric sizes (such as M12*1.0, M14*1.25), and micro-taps (down to M1.0) with customized pitch diameter tolerances (6H, 6G, 4H) tailored to your drawing requirements.

Elevate Your Production Yield with Enterprise Threading Tools

Connect directly with our tooling engineers to request custom catalogs, technical data sheets, or wholesale price quotations for your Seoul manufacturing operations.

Send an Inquiry